
The 2026 Top Shuttle Rotomolding Machine Types for Buyers guide examines equipment choices through practical production needs. A Shuttle Rotomolding Machine uses separate stations for heating, cooling, loading, and unloading. This arrangement can reduce idle time when operators plan each movement carefully. In a working plant, mold size, resin volume, oven temperature, and cooling airflow shape real output. Catalog capacity alone rarely tells the complete story.
This introduction focuses on shuttle machines for water tanks, industrial containers, playground parts, and custom hollow products. Buyers should compare carriage payload, mold-change speed, PLC controls, burner or electric heating, and cooling consistency. Ask manufacturers for cycle records, energy data, service response times, and references from similar factories. Experienced suppliers should explain how wall thickness, part geometry, and powder quality affect production stability. Small details matter. A loose thermocouple can distort process decisions. Poor ventilation can also increase operating costs. Independent testing is valuable when claims appear unusually optimistic.
The guide also considers single-arm and multi-arm configurations, compact systems, and larger automated lines. Each type has trade-offs involving floor space, labor, flexibility, and maintenance. No machine fits every buyer. That is worth remembering. Some performance comparisons remain uncertain without trials using the buyer’s actual molds and materials. A careful purchasing decision should combine engineering advice, documented evidence, operator feedback, and total ownership costs. This approach supports safer planning and more dependable long-term production.
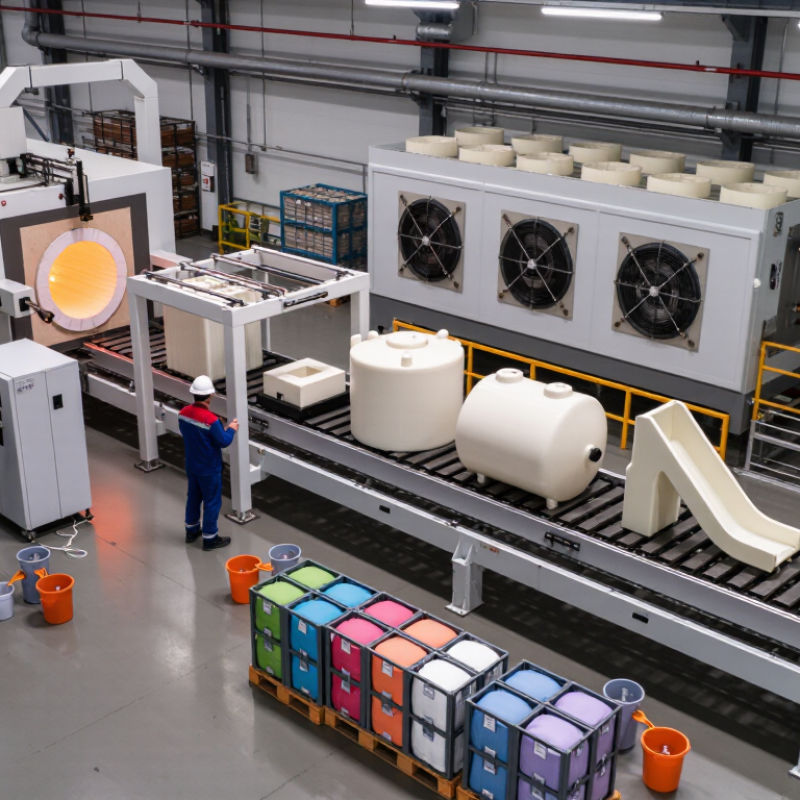
A shuttle rotomolding machine uses two perpendicular axes to rotate a mold inside a heated oven. Polyethylene powder melts against the mold wall during this movement. The shuttle carriage then moves to a cooling station, while another carriage can begin heating. That separation supports flexible production. A typical cycle includes mold loading, oven heating, controlled rotation, cooling, and part removal. Operators should check powder distribution before every cycle. Small clumps can create thin corners, trapped air, or uneven wall thickness.
Plastics Europe’s Plastics—the Fast Facts 2024 report recorded 413.8 million tonnes of global plastics production in 2023. Rotational molding serves smaller but important applications, including tanks, containers, playground parts, and industrial housings. Grand View Research’s 2024 market analysis projects roughly 4.7% annual growth for the rotational molding sector through the decade. The figure is useful, but not a buying guarantee. Control matters more than speed. Oven temperature, mold rotation ratio, cooling airflow, and powder mass must work together. A practical operator records cycle temperature and part weight, then compares them with defects. That motion matters.
Cooling is often underestimated. Excessive airflow may warp a large panel, while slow cooling can extend the cycle unnecessarily. Manual judgment still affects results. Control is imperfect. Even experienced teams should validate new molds through trial cycles, cross-sectional checks, and dimensional measurements before routine production.
| Machine Type | Basic Configuration | Typical Mold or Product Size | Common Materials | Suitable Applications | Core Operating Principle | Key Advantages | Buyer Considerations |
|---|---|---|---|---|---|---|---|
| Single-Station Shuttle Machine | One mold carriage moves between the heating chamber and the cooling or loading area. | Small to medium hollow parts; size depends on the chamber and carriage dimensions. | Polyethylene, cross-linked polyethylene, polypropylene, polyamide, and selected engineering resins. | Tanks, containers, planters, toys, housings, and agricultural components. | Plastic powder is loaded into a mold. The carriage enters a heated chamber and rotates on two perpendicular axes so the softened polymer coats the mold wall. The mold then moves out for controlled cooling. | Simple layout, moderate investment, flexible mold changes, and easy access for manual loading. | Production output is limited by the single mold cycle; labor and cooling control should be assessed carefully. |
| Two-Station Shuttle Machine | Two mold carriages or two working positions share a heating chamber and a cooling or loading zone. | Small, medium, or large parts depending on oven width, carriage capacity, and mold envelope. | Rotomolding-grade polyethylene is most common; other compatible thermoplastics may be used after process validation. | Storage tanks, road barriers, industrial containers, ducts, and medium-sized technical parts. | One carriage is heated while the other is unloaded, loaded, or cooled. Each mold rotates biaxially during heating to distribute material without internal pressure. | Better utilization of the oven, shorter idle time, and higher productivity than a basic single-station layout. | Requires accurate timing between heating, transfer, cooling, and mold preparation operations. |
| Independent Double-Shuttle Machine | Two shuttles operate independently, allowing different molds or products to follow separate cycle schedules. | Mixed-size production, from compact parts to large rotationally molded components. | Polyethylene grades, polypropylene, polyamide, and other thermoplastics approved for rotational molding. | Manufacturers producing several product sizes, replacement parts, bins, tanks, and customized components. | Each shuttle can be positioned and timed separately. Biaxial rotation continues during the heating stage, while independent cooling parameters help accommodate different wall thicknesses. | High scheduling flexibility, improved equipment utilization, and reduced disruption when molds or products change. | Higher control-system complexity and greater floor-space requirements than a basic shuttle arrangement. |
| Multi-Arm Shuttle Machine | Several mold arms or carriages move between a common heating chamber and separate service areas. | Medium to large parts, or multiple smaller molds loaded on one arm. | Most commonly rotational-molding polyethylene and other thermoplastics with suitable melt-processing behavior. | Large containers, pallets, seating products, playground components, and industrial equipment covers. | Molds are heated while rotating around two axes. Multiple arms are sequenced so heating, cooling, demolding, and loading activities can overlap. | Higher throughput, better use of oven capacity, and the ability to run multiple mold configurations. | Arm payload, interference clearance, oven uniformity, and maintenance access must be checked before purchase. |
| Large-Part Shuttle Machine | Heavy-duty shuttle carriage with a large oven and reinforced rotation system for oversized molds. | Large tanks, cabins, containers, ducts, and other hollow products with substantial mold dimensions. | Primarily polyethylene; material selection depends on impact, chemical, temperature, and structural requirements. | Water and chemical tanks, traffic products, marine components, agricultural tanks, and large housings. | A measured polymer charge is placed inside the mold. Heat softens the polymer while controlled biaxial rotation builds a hollow wall. Cooling solidifies the part before demolding. | Supports large products with relatively low tooling pressure and can produce seamless hollow structures. | Higher energy demand, longer heating and cooling times, heavy mold handling, and stricter foundation requirements. |
| Electric-Drive Shuttle Machine | Electric motors and electronically controlled drives operate arm rotation, carriage movement, and auxiliary functions. | Small to large products, subject to motor torque, arm payload, and oven dimensions. | Compatible with standard rotational-molding thermoplastics when the machine provides suitable process temperatures. | Precision parts, repeat production, containers, technical housings, and applications requiring process data recording. | Programmable drive systems control rotational speed, axis ratio, heating time, cooling time, and movement sequences. Rotation remains coordinated while the polymer melts and coats the mold. | Accurate speed control, clean operation, reduced hydraulic-oil use, and easier recipe repeatability. | Electrical infrastructure, drive protection, software support, and replacement-part availability should be evaluated. |
| Hydraulic-Drive Shuttle Machine | Hydraulic motors and cylinders provide carriage movement, arm rotation, clamping, or auxiliary actuation. | Medium to large products where high torque and heavy-duty movement are required. | Common rotational-molding thermoplastics, including various polyethylene grades. | Heavy tanks, industrial containers, large molds, and demanding production environments. | Hydraulic power transfers torque to the rotating arms and moves the shuttle carriage. Heating melts the charge, while biaxial rotation distributes the material over the mold surface. | High torque capability, robust movement, and suitability for heavy molds and large equipment. | Hydraulic-temperature control, leakage prevention, filtration, noise, and maintenance costs require attention. |
| Gas-Fired Shuttle Machine | A combustion heating system supplies hot air to the oven through a controlled burner and circulation system. | Medium to large products, depending on thermal capacity and oven volume. | Thermoplastics selected for the required processing window, especially rotational-molding polyethylene. | Large tanks, bins, barriers, agricultural products, and general-purpose hollow components. | Controlled hot air transfers heat to the mold and polymer charge. Biaxial mold rotation promotes even coating, while sensors and controls manage the thermal cycle. | High heating capacity and suitability for large ovens and heavy molds. | Ventilation, combustion safety, fuel supply, exhaust management, and temperature uniformity are essential. |
| Electric-Heated Shuttle Machine | Electrical heating elements and circulation fans create and distribute hot air inside the oven. | Small to medium products, with larger configurations available for higher electrical capacity. | Polyethylene and other thermoplastics that meet the machine's temperature range and process requirements. | Indoor production, technical parts, containers, small tanks, and operations requiring clean heating. | Heating elements raise the oven-air temperature. The rotating mold transfers heat to the polymer charge, which melts and forms a continuous hollow layer against the mold wall. | Clean operation, straightforward temperature control, and no combustion exhaust at the machine. | Electrical load, heating-element replacement, insulation quality, and operating cost should be compared with fuel-based systems. |
| Automated Shuttle Rotomolding Cell | Shuttle equipment is integrated with automated dosing, mold handling, temperature monitoring, cooling, and demolding functions. | Repeated production of small, medium, or large parts, depending on cell design. | Validated rotational-molding thermoplastics, with material handling matched to powder size and formulation. | High-volume containers, repeatable industrial parts, automotive components, and products with strict process records. | Automated systems control the material charge, mold movement, biaxial rotation, heating profile, cooling sequence, and production data collection. | Consistent cycle control, lower manual handling, improved traceability, and potential labor savings. | Higher initial investment; integration, programming, safety guarding, and operator training are critical. |
| Manual or Semi-Automatic Shuttle Machine | Operators manually load powder, install molds, monitor selected steps, and remove finished parts; movement may be powered. | Small to medium products and low-to-moderate production volumes. | Common rotational-molding powders, especially polyethylene grades suitable for the mold and cycle. | Prototypes, custom parts, short production runs, replacement components, and frequent mold changes. | The operator prepares the mold and charge, while the machine performs controlled heating and biaxial rotation. Cooling and demolding are completed according to the production procedure. | Lower entry cost, flexible production, and practical for varied or low-volume products. | Output and consistency depend more heavily on operator skill, work instructions, and process monitoring. |