Request a free quote Phone Icon
die cutting materials

Blog

How to Choose the Right Deep Hole Honing Machine?

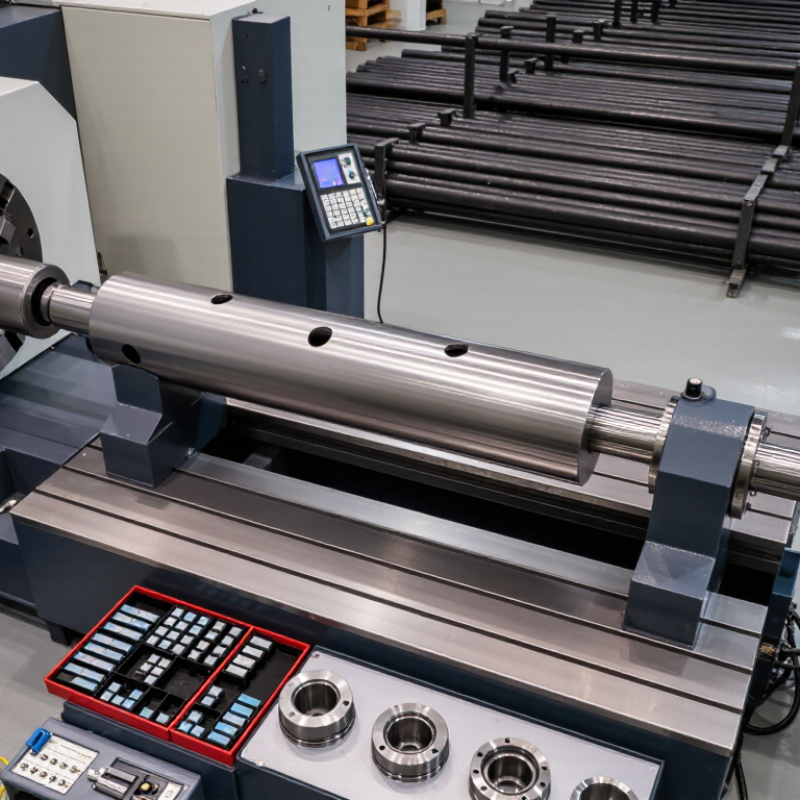
Choosing a Deep Hole Honing machine begins with the part, not the brochure. Bore diameter, length, material, and starting condition all shape the decision. A long steel tube with a narrow bore demands different tooling and support than a short hydraulic cylinder. Small details matter.

A reliable recommendation also needs a verified technical source. No expert name or quotation was provided, and I cannot confirm a suitable published statement here. Rather than invent an attribution, this draft leaves a clear place for one: “[Verified expert name] said, ‘[Verified quotation about Deep Hole Honing machine selection].’” Add the quotation only after checking its source and wording.

Then compare machines against measurable needs. Can the spindle maintain alignment across the full bore? Does the system control stone pressure, stroke, and coolant flow? Look for practical evidence, such as sample parts, bore measurements, surface-finish reports, and a clear tooling plan. Ask how operators will handle setup and repeat production. A machine may look capable on paper. The test part tells more.

This guide will explain how to weigh accuracy, capacity, automation, tooling, service, and total operating cost. It will also point out where specifications can mislead. A larger machine is not automatically the better choice. And the cheapest quote may leave important tooling or support costs out. The right machine should fit the work today, while allowing room for realistic production changes.
How to Choose the Right Deep Hole Honing Machine?

Define the Deep Hole Honing Task and Required Bore Geometry

How to Choose the Right Deep Hole Honing Machine?

Define the Deep Hole Honing Task and Required Bore Geometry

Start with the bore, not the machine. Record its diameter, depth, and whether it is blind or through. Note the workpiece material and the amount of stock that must be removed. These details affect tool reach, honing stroke, and workpiece support. For example, a long, slender bore may need careful alignment to limit deflection. A blind bore also requires attention to tool clearance at its closed end.

Tips: Measure several points along the bore, not just the opening. Check roundness, straightness, and the required surface finish. Note any cross-holes, shoulders, or changes in diameter. These features can interrupt tool contact or limit access. Keep the measurement method with the drawing; dimensions without tolerances leave room for guesswork.

Confirm that the machine can cover the full working length and diameter range, including the tool’s entry and exit space. Consider how the part will be clamped and aligned, especially if it is heavy or awkward to handle. Don’t assume a nominal bore size tells the whole story. A bore that looks simple on a drawing may behave differently after setup. Recheck critical dimensions on the actual part when possible; measurement variation is easy to underestimate.
Assess Workpiece Material, Dimensions, and Production Volume

Match the machine to the material before comparing spindle power. The ASM Handbook, Volume 1, gives typical room-temperature thermal expansion values near 12 µm/m·°C for carbon steel and 23 µm/m·°C for aluminum; exact values vary by alloy. Heat matters. For long bores, even modest temperature changes can affect measurements, so consider coolant control and when parts are gauged. Hard or abrasive materials may also need different stone specifications and lower cutting rates.

Record bore diameter, length, length-to-diameter ratio, starting stock, and required finish. A 40 mm bore that is 800 mm deep needs more attention to tool guidance and bar deflection than a short, wide bore. Check the machine’s usable stroke and fixture clearance against the actual part, not just its maximum advertised capacity. I would also verify clamping distortion on thin-walled parts; it is easy to overlook.

Production volume changes the economics. For 1,000 parts monthly, a five-minute honing cycle alone requires about 83 machine hours, before loading, inspection, and changeovers. That estimate is only a starting point. Compare it with available shifts, batch sizes, and realistic setup time. A higher-capacity machine may be unnecessary for intermittent work, while frequent changeovers can make a faster cycle less valuable than expected.

How to Choose the Right Deep Hole Honing Machine? — Assess Workpiece Material, Dimensions, and Production Volume
Workpiece and Material Typical Bore Dimensions Production Volume Machine Configuration to Consider Key Selection Checks
Steel hydraulic cylinder tube Inside diameter: 40–150 mm
Length: 1–6 m
Low to medium; frequent changes in tube size or length Horizontal machine with adjustable supports, through-bore capability, and a stroke suited to the longest part Confirm maximum workpiece length, support spacing, bar rigidity, and the required bore finish. Long tubes need adequate support to limit deflection.
Cast iron engine or compressor cylinder Inside diameter: 70–180 mm
Length: 100–500 mm
Medium to high; repeated parts and stable process conditions Vertical or horizontal machine with repeatable fixturing and programmable stroke and dwell settings Check casting variation, bore alignment, stock allowance, and whether the machine can consistently produce the specified crosshatch and geometry.
Stainless steel process tube Inside diameter: 25–100 mm
Length: 0.5–4 m
Low to medium; material grades and dimensions may vary Horizontal machine with adjustable tooling and controlled honing-fluid delivery Verify abrasive compatibility, coolant filtration, corrosion control, and the ability to prevent heat buildup or surface damage.
Aluminum alloy sleeve or housing Inside diameter: 20–80 mm
Length: 50–400 mm
Medium to high; often batch production Compact vertical or horizontal machine with accurate workholding and adjustable pressure Use a process suited to the alloy and required finish. Check clamping force to avoid distorting thin walls and confirm reliable chip and abrasive removal.
Hardened steel hydraulic or precision component Inside diameter: 10–60 mm
Length: 100–1,000 mm
Low to medium; tight tolerances or high-value parts Precision machine with rigid tooling, controlled feed, and in-process or frequent bore measurement Assess hardness, initial bore condition, stock removal, roundness and straightness requirements, and the measurement method used for process verification.
Long, small-diameter bore in steel or alloy Inside diameter: 8–30 mm
Length: 0.5–3 m
Low to medium; setup stability is especially important Deep-stroke horizontal configuration with a suitably long honing tool and support for the workpiece and tool Check the bore length-to-diameter ratio, tool reach and stiffness, alignment, coolant access, and the risk of tool deflection or vibration.
Mixed-material job shop work Inside diameter: 15–200 mm
Length: 100 mm–6 m
Low volume; frequent changes in part family Flexible machine with interchangeable tooling, adjustable supports, and a broad usable stroke and diameter range Compare the actual part range with the machine’s rated limits. Consider changeover time, tooling availability, operator access, and the number of setups required.

The dimensions and production categories are practical screening examples, not universal machine limits. Confirm the required bore diameter, stroke, workpiece weight, tolerance, surface finish, and tooling range with the machine specification and a representative part trial.

Match Machine Capacity, Accuracy, and Honing Technology to the Job

How to Choose the Right Deep Hole Honing Machine?

Match the machine’s working envelope to the part, not just its nominal bore diameter. Check maximum stroke, workpiece length, clamping clearance, and tool expansion range. A 40 mm bore may need a longer stroke than expected when the component is narrow but deep. The 2023 Gardner Intelligence World Machine Tool Survey reported global machine-tool consumption of about $98 billion for 2022, highlighting the scale of capital investment across manufacturing. For your own purchase, compare verified cycle times and maintenance needs, not market size alone. Fit matters.

Accuracy depends on the complete setup. Ask suppliers to demonstrate roundness, straightness, and surface finish on a representative workpiece, using your measurement method. Specify the required tolerances before choosing controls or spindle options. A machine’s stated capability is not a guarantee under every abrasive, material, or operator condition. This detail is easy to overlook. Match honing technology to the job: single-pass systems can suit stable, repeat production, while conventional honing offers flexibility for varied bores and correction needs.

Tips: Bring a sample part and define acceptable results in writing. Request a repeatability trial across several parts, then inspect tool wear and cycle time. A catalog number can still mislead; real parts sometimes reveal awkward setup limits.

Compare Tooling, Controls, Automation, and Maintenance Requirements

Tooling should match the bore, not just the machine’s advertised capacity. Check workpiece length, diameter, material, stock allowance, and required finish. A long, slender bore may need different support and stone pressure than a short steel sleeve. Ask for a trial on representative parts. The result can reveal chatter or uneven contact that a specification sheet misses.

Controls affect repeatability. Look for adjustable spindle speed, stroke length, and honing pressure, plus clear alarms and stored job settings. Operators should be able to change a recipe without hunting through menus. Keep setup practical. Automation can load parts, measure bores, or sort finished components, but it adds sensors and integration work. For low-volume production, a skilled operator and simple gauging may be more dependable.

Maintenance deserves a close look before purchase. Check access to the honing head, stone holders, filters, and coolant tank. Ask how often stones, seals, and guides typically need inspection under similar operating conditions. These intervals vary with material and production rate, so avoid relying on a single estimate. Request a maintenance demonstration, then note how long a routine change takes. It is easy to overlook cleanup time. That matters on a busy shift.

Evaluate Safety, Support, and Total Cost Before Selecting a Machine

Choosing a deep hole honing machine starts with the work area, not the brochure. Check that operators can load long, heavy workpieces without awkward reaches. Inspect the guard, door interlocks, emergency stops, and coolant containment in person. Small details matter. The U.S. Bureau of Labor Statistics reported 2.8 recordable injury and illness cases per 100 full-time workers in manufacturing in 2023. That figure is not machine-specific, but it reinforces the need to review safe access, training, and maintenance procedures before purchase.

Support deserves the same scrutiny as cutting performance. Ask who diagnoses faults, how quickly technicians respond, and which wear parts are kept in stock. Request a sample service plan covering honing stones, mandrels, filtration, and operator training. Deloitte’s 2024 Smart Manufacturing survey found that 92% of surveyed manufacturers viewed smart manufacturing as a driver of competitiveness. For a honing cell, useful connectivity means actionable alarms and accessible service data—not dashboards no one checks.

Compare total cost over the machine’s expected working life. Include installation, floor preparation, tooling, coolant, energy, calibration, and planned downtime. A low purchase price can look less attractive when a worn mandrel delays a production run. Ask suppliers to demonstrate a representative bore and record cycle time, finish, and tool consumption. Then question your own assumptions: one successful sample is not proof of stable production. A spreadsheet can miss that.